Whether a plant is new or decades old, MES has the same job: govern execution, record product history and connect the shop floor to the business. What differs is where the constraints come from.
Greenfield: specify before you buy
In a new plant, the biggest opportunity is timing. Equipment interfaces, signal lists, identification points and network requirements can be written into OEM purchase orders. MES can be designed alongside the process, so the plant goes live with execution governance rather than adding it years later.
- Define the digital architecture early.
- Specify interfaces in every equipment order.
- Plan identification and inspection points with the process design.
- Commission MES with the lines, not after them.
Brownfield: connect what exists
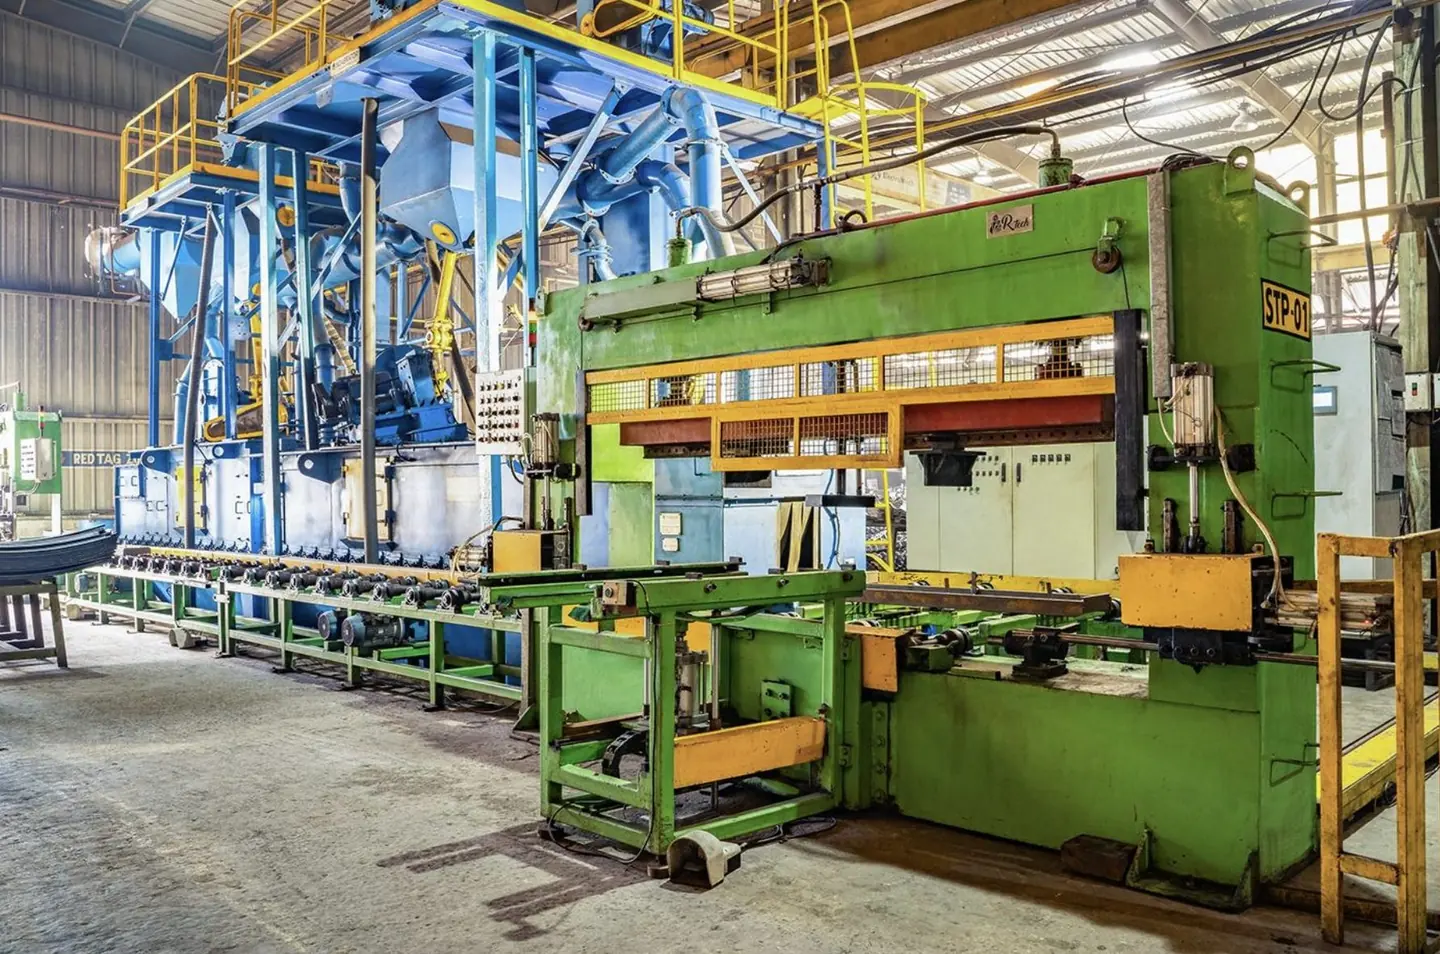
In a running plant, the starting point is a mix of machines, controls, records and habits. The priority is to understand that reality, connect what can be connected, make losses visible and introduce governance in phases that production can absorb.
- Start with an assessment or blueprint.
- Use quick visibility wins to build confidence.
- Phase MES by area or process.
- Replace equipment only where it is genuinely the better option.
In both cases, the order of work matters more than the software: understand the factory, improve the process, connect the systems, then govern execution.