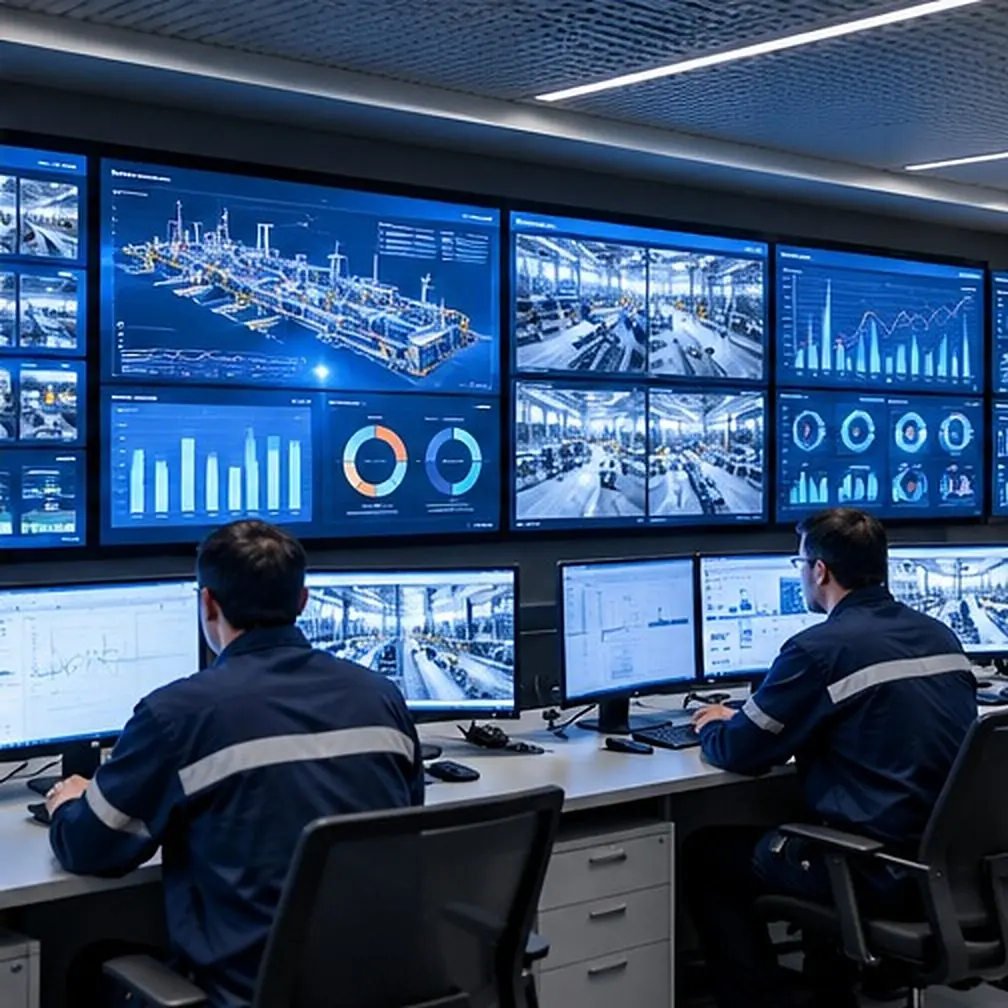
Turning industrial data into intelligent decisions
Connected machines and digital systems create visibility. Industrial AI takes the next step, helping manufacturers predict problems, optimise operations and make better decisions.
Powered by our strategic AI partner, Algo8
Vector11 delivers the foundation through industrial automation, connectivity, performance monitoring and SMART MES.
Together with Algo8’s Industrial AI capabilities and PlantBrain platform, we help manufacturers progress from connected operations to predictive intelligence, intelligent optimisation and governed autonomy.
Connected operations
Machines, controls and systems connected, giving reliable data from the shop floor.
Predictive intelligence
AI spots failures, quality drift and losses before they disrupt production.
Intelligent optimisation
Models recommend better schedules, settings and energy use.
Governed autonomy
Proven decisions automated within clear rules and human oversight.
Explore selected use cases
From discrete manufacturing to process industries, energy and supply chains, discover how AI can address real operational challenges and improve business performance.
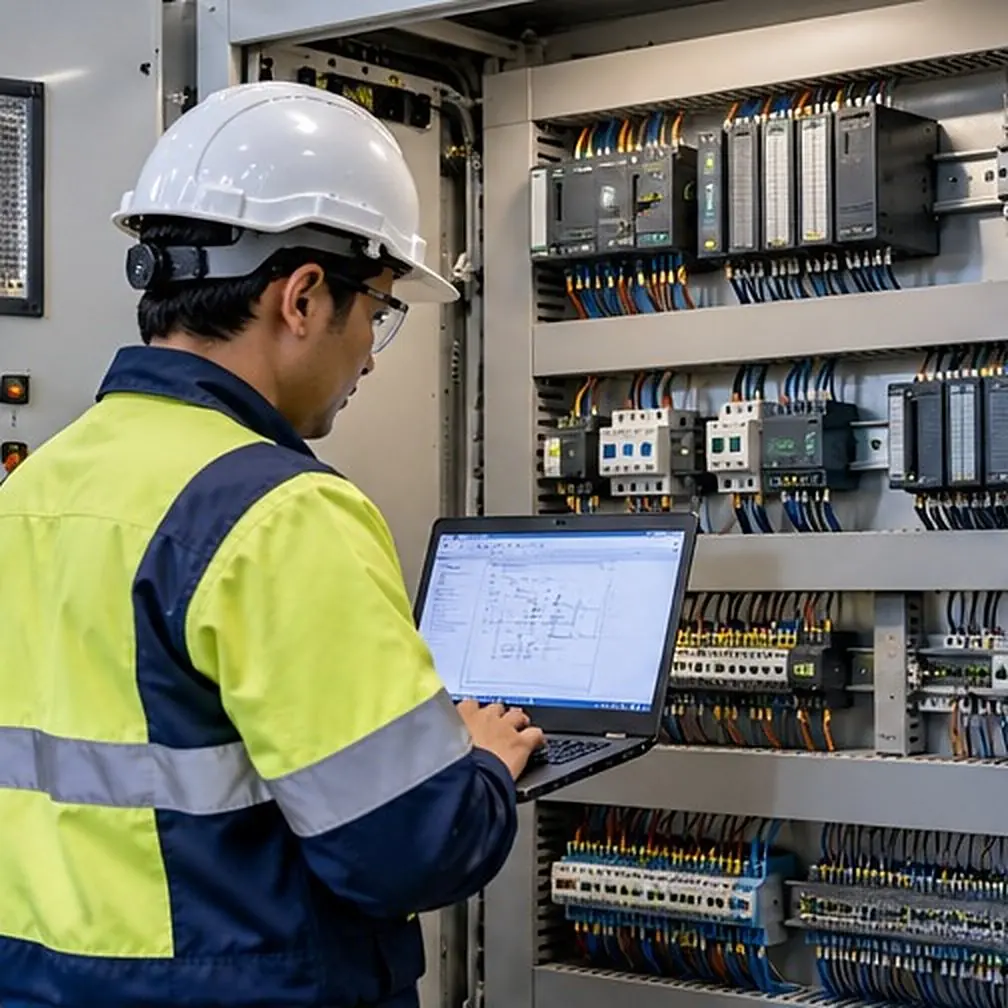
Predictive maintenance & asset reliability
Anticipate failures before they disrupt production.
AI analyses equipment conditions, vibration, temperature and operating patterns to identify early signs of deterioration and predict potential failures.
Business impact
- Reduced unplanned downtime
- Improved equipment reliability
- Optimised maintenance costs
- Longer asset life
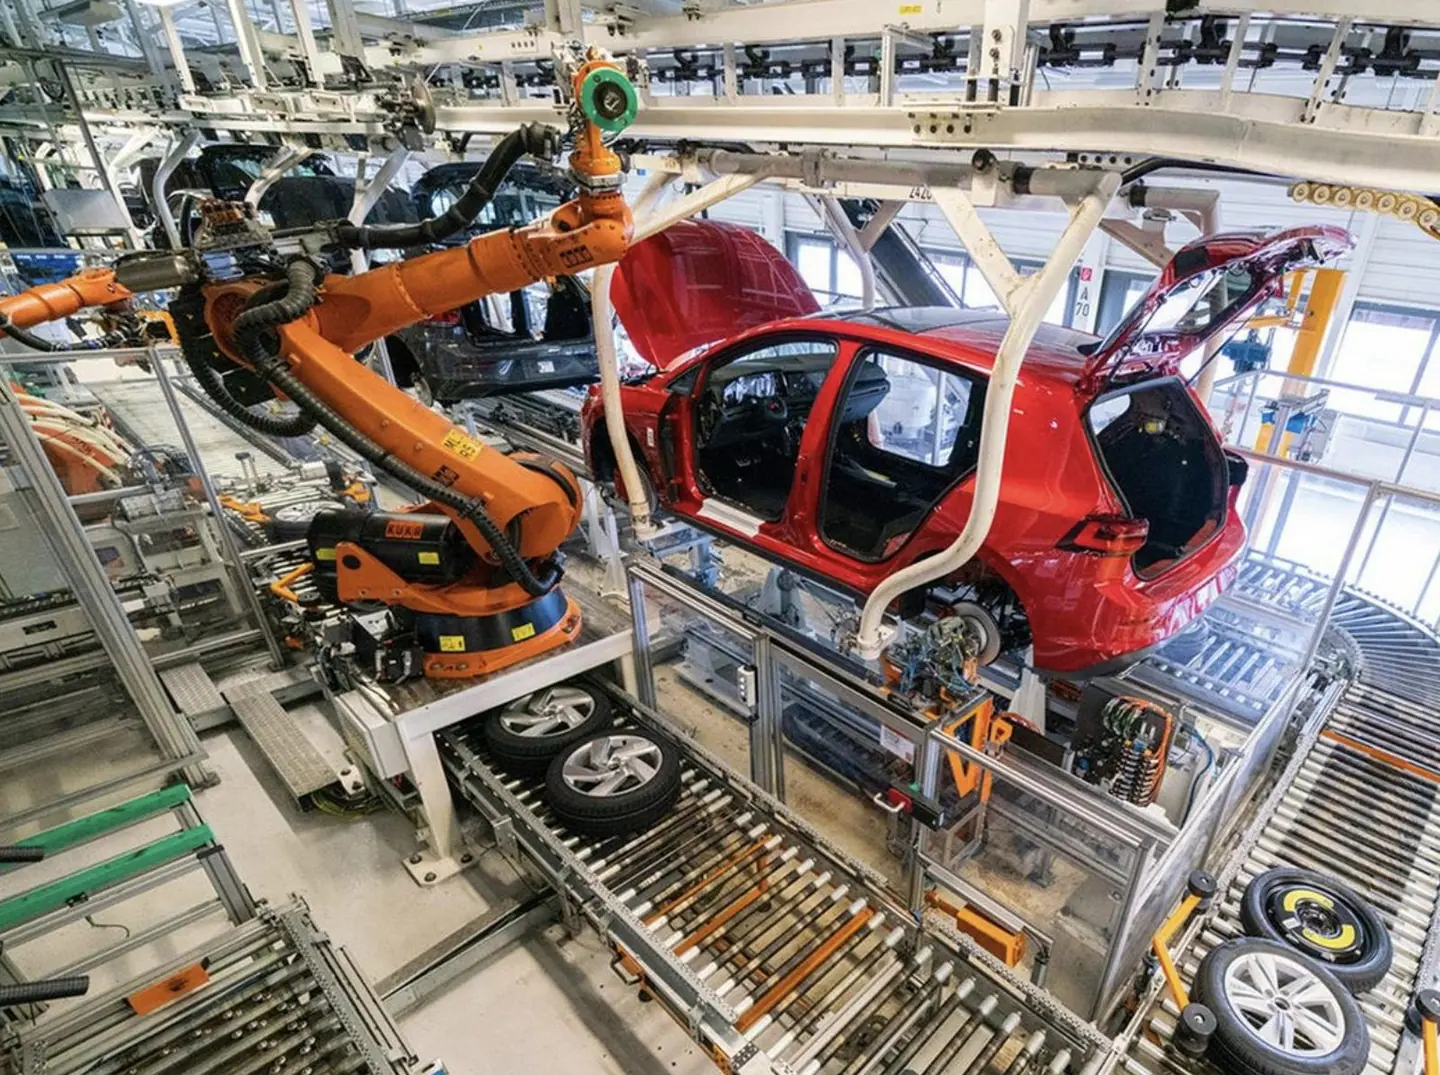
Intelligent production planning & scheduling
Make production plans that adapt to real-world conditions.
AI dynamically optimises production schedules based on machine availability, material readiness, production capacity and changing priorities.
Business impact
- Higher throughput
- Improved on-time delivery
- Reduced work-in-progress
- Better resource utilisation
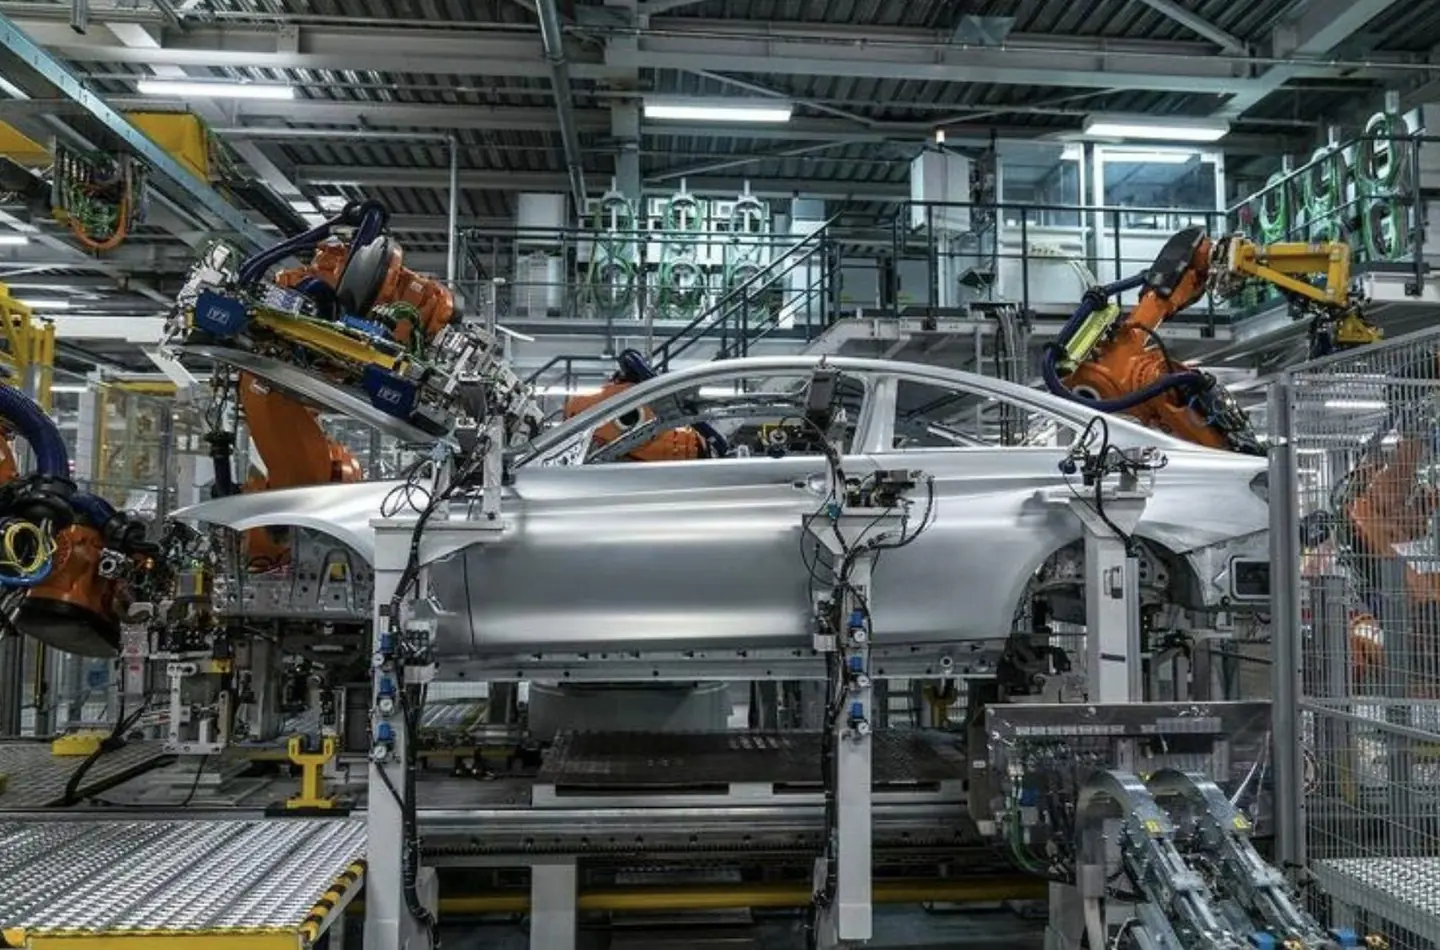
AI-powered visual quality inspection
Detect quality problems faster and more consistently.
Industrial computer vision identifies surface defects, product variations and process abnormalities in real time, enabling early corrective action and reducing dependence on manual inspection.
Business impact
- Improved first-pass yield
- Reduced scrap and rework
- More consistent product quality
- Faster inspection
Energy & process optimisation
Use energy intelligently. Improve process performance.
AI combines operational data, energy consumption patterns and predictive models to identify inefficiencies, forecast energy demand and recommend optimised operating conditions.
Business impact
- Lower energy costs
- Reduced process losses
- Improved resource efficiency
- Better environmental performance
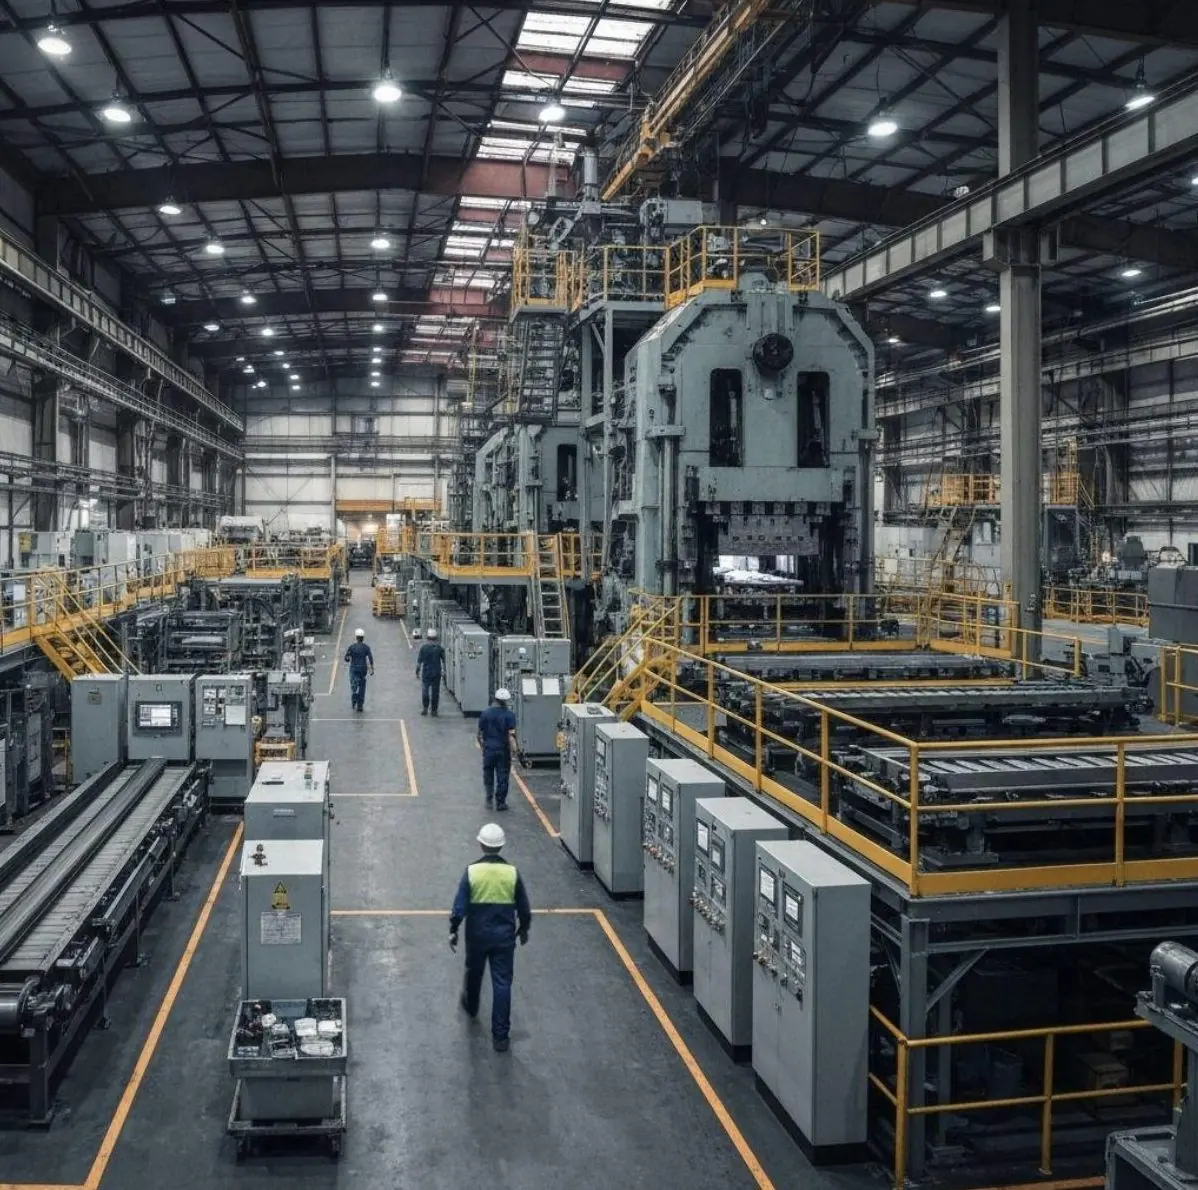
AI-powered industrial safety
Move from reactive safety monitoring to proactive risk detection.
Computer vision monitors PPE compliance, hazardous-area access, vehicle movements and unsafe operating conditions, generating real-time alerts for faster intervention.
Business impact
- Stronger safety compliance
- Quicker response to unsafe conditions
- Reduced workplace risks
Demand forecasting & supply chain intelligence
Connect demand, inventory and production decisions.
AI integrates historical demand, inventory levels, supplier information and operational constraints to improve forecasting, material planning and replenishment decisions.
Business impact
- Improved forecast accuracy
- Optimised inventory
- Reduced stockouts
- Improved working-capital efficiency
From industrial connectivity to enterprise intelligence
Vector11 and Algo8 bring complementary strengths to industrial transformation.
Vector11
Specialises in industrial automation, IIoT, plant connectivity, equipment performance, SMART MES and enterprise intelligence.
Algo8
Specialises in advanced industrial AI, including PlantBrain, predictive maintenance, asset reliability, predictive quality, process optimisation and intelligent decision support.
Together, these capabilities create a practical path from shop-floor connectivity to enterprise-wide intelligence.
About our strategic partnership
Discover what industrial AI can do for your business
These are just a few examples of the possibilities.
Our strategic AI partner, Algo8, offers a wider portfolio of industrial AI solutions through its PlantBrain platform, helping enterprises improve operational performance and move toward intelligent, increasingly autonomous operations.
Discover more use cases, technologies and industrial AI solutions.